Custom Aluminum Extrusion Manufacturers: Explore Design and Process Options
Custom aluminum extrusion manufacturers support industries that need metal profiles shaped around specific engineering and functional requirements. Unlike standard profiles, custom extrusions can be developed around particular dimensions, tolerances, structural needs, and assembly methods.
The extrusion process is especially useful when a component must combine strength, controlled geometry, low weight, and repeatable production. Aluminum's ability to form complex cross-sections also allows engineers to integrate features such as channels, ribs, mounting points, and internal cavities into a single profile.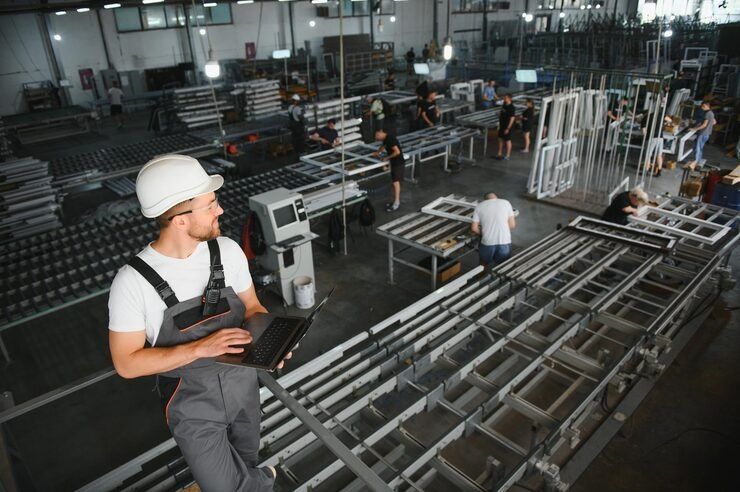
Understanding the design and manufacturing choices behind custom extrusions helps engineers, product developers, architects, and procurement teams evaluate whether an aluminum profile is appropriate for a particular application. The process involves far more than pressing metal through a shaped opening, with material selection, die engineering, finishing, and post-extrusion fabrication all affecting the final result.
How Custom Aluminum Extrusion Begins With Product Design
The first stage is translating a functional requirement into a manufacturable cross-section. Engineers consider the loads the component will experience, how it will be assembled, its environmental exposure, and the dimensional accuracy required during operation.
A well-designed profile uses aluminum efficiently while providing the needed structural properties. Wall thickness, corner radii, hollow sections, openings, and transitions all influence how smoothly material can flow through the extrusion die.
Designers also consider manufacturability from the beginning. Very thin walls, abrupt thickness changes, and highly uneven sections can make extrusion more difficult and may affect dimensional consistency. A balanced cross-section generally supports more predictable metal flow.
Computer-aided design software is commonly used to model profiles before tooling is created. This allows teams to evaluate geometry, identify potential interference with adjacent parts, and refine the design before production begins.
Choosing the Right Aluminum Alloy
All aluminum alloys do not behave identically during extrusion. Alloy selection depends on the balance required among strength, formability, corrosion resistance, surface appearance, and intended use.
Common extrusion alloys include 6061 and 6063, although many other alloy families are available for specialized requirements. The 6063 family is widely associated with profiles where surface quality and extrusion characteristics are important, while 6061 is often selected when higher mechanical strength is a priority.
Temper also matters because heat treatment and processing conditions influence mechanical properties. Engineers therefore need to consider both alloy and temper rather than selecting aluminum based only on its broad material designation.
The correct combination allows manufacturers to align material behavior with the intended performance of the finished component.
Die Design Determines Profile Geometry
The extrusion die is one of the most important elements in custom profile manufacturing. It contains the opening that determines the cross-sectional shape of the extruded material.
A simple solid profile may require relatively straightforward tooling, while hollow or multi-featured profiles can require more complex die arrangements. Internal cavities, narrow channels, and varying wall thicknesses increase the engineering considerations involved in maintaining stable material flow.
Die design also influences tool life and dimensional stability. Engineers analyze how aluminum moves through the tooling to reduce imbalances that could produce distortion, uneven dimensions, or surface defects.
For this reason, close communication between product designers and extrusion specialists can be valuable before finalizing the profile geometry.
The Core Extrusion Process
Once the design and tooling are prepared, aluminum billets are heated to a controlled temperature suitable for extrusion. The softened billet is then pushed through the die, producing a continuous profile with the required cross-section.
The emerging material is cooled and guided along the production line. Straightening or stretching may be used to improve dimensional alignment before the profile is cut into specified lengths.
Depending on the alloy and required properties, heat treatment may follow extrusion. This stage can improve mechanical strength and help the finished component meet its intended performance requirements.
Although the basic process appears straightforward, temperature control, extrusion speed, tooling condition, and cooling behavior all influence profile quality.
Design Features That Can Be Integrated Into an Extrusion
One major advantage of custom extrusion is the ability to combine several functional features within one profile.
A component may be designed with:
- Mounting grooves for assembly hardware
- Channels for wiring or tubing
- Ribs for additional stiffness
- Slots for adjustable connections
- Internal cavities to reduce mass
- Flanges for joining adjacent components
- Specialized surfaces for later machining or finishing
Integrating these features can reduce the number of separate pieces required in an assembly. It may also simplify alignment because multiple functions are incorporated directly into the aluminum profile.
However, additional geometry should serve a clear engineering purpose. Unnecessary complexity can make tooling more difficult and may complicate downstream fabrication.
Surface Finishing Changes Appearance and Performance
After extrusion, aluminum profiles can receive surface treatments selected according to their operating environment and visual requirements.
Anodizing is commonly used to create a durable oxide layer that can improve surface characteristics and provide decorative finishes. Powder coating can provide a broad range of surface appearances while adding another layer of protection.
Other finishing approaches may be appropriate for specialized industrial requirements. The choice depends on exposure conditions, abrasion, corrosion considerations, color requirements, and dimensional tolerances.
Surface treatment also needs to be considered during the design stage because finishing can influence final dimensions, particularly in tight-tolerance applications.
Fabrication After Extrusion
An extruded profile does not always represent the completed component. Secondary fabrication can transform a continuous extrusion into a finished assembly-ready part.
Common operations include cutting, drilling, tapping, milling, punching, bending, and specialized machining. Precision machining can create holes, slots, mounting surfaces, and other features that cannot be formed economically through the initial extrusion geometry.
Fabrication should be planned alongside extrusion rather than treated as a completely separate activity. Profile orientation, access for cutting tools, tolerances, and clamping requirements can all influence the most practical manufacturing sequence.
Managing Tolerances and Quality
Dimensional consistency is critical when custom aluminum profiles must fit with other engineered components. Extrusion tolerances are influenced by profile geometry, alloy, tooling, process conditions, cooling, and subsequent straightening.
Manufacturers may use dimensional inspection, surface inspection, mechanical testing, and other quality-control methods depending on application requirements.
For complex components, technical drawings should clearly identify critical dimensions and tolerances. Not every measurement requires the same level of precision, and distinguishing critical features from non-critical ones can help establish a realistic manufacturing specification.
Material traceability and documented quality procedures can also be important when extrusions are used in regulated or technically sensitive industries.
Where Custom Aluminum Extrusions Are Used
The flexibility of aluminum extrusion makes the process suitable for many applications. Building systems may use profiles for framing, curtain wall components, architectural structures, and specialized enclosures.
Industrial equipment can incorporate extrusions into machine frames, guards, heat-management assemblies, conveyors, and automated systems. Transportation applications can benefit from lightweight structural sections, while electronics may use precisely designed profiles for housings and thermal management.
Renewable energy equipment also uses aluminum profiles in structures where corrosion resistance, low mass, and repeatable geometry are valuable.
The appropriate extrusion design ultimately depends on the loads, environment, assembly requirements, and manufacturing constraints of the specific application.
How to Evaluate a Custom Extrusion Project
A successful extrusion program usually begins with a complete technical definition rather than an isolated profile drawing. Engineers should identify the functional purpose of the component, expected loads, joining method, environmental conditions, and critical dimensional requirements.
Tooling considerations should be reviewed early, especially when the profile includes hollow sections, thin walls, or significant geometric variation.
It is also useful to evaluate the complete manufacturing route, including extrusion, heat treatment, finishing, machining, inspection, and final assembly. Looking at the whole process helps prevent a profile from being optimized for extrusion while creating unnecessary difficulties later.
Frequently Asked Questions
What makes an aluminum extrusion “custom”?
A custom aluminum extrusion is developed around a specific cross-sectional geometry rather than a standard stock profile. The design can incorporate application-specific dimensions, channels, cavities, ribs, slots, and mounting features.
Which aluminum alloy is commonly used for custom extrusion?
Alloy selection depends on the application's requirements. 6063 is widely associated with extrusion-friendly profiles and surface appearance, while 6061 is often considered where greater mechanical strength is required.
Can custom extrusions include holes and mounting features?
Yes, but there is a distinction between features formed directly into the extrusion and those created through secondary fabrication. Drilling, milling, punching, and tapping can add features after extrusion when they are not practical to include in the profile itself.
What factors influence extrusion tolerances?
Profile geometry, alloy, die condition, extrusion temperature, production speed, cooling, and straightening can all affect dimensional results. Critical tolerances should therefore be identified clearly during engineering and quality planning.
What finishing methods can be applied to aluminum extrusions?
Common finishing methods include anodizing and powder coating. The appropriate treatment depends on appearance, environmental exposure, surface durability, and dimensional requirements.
Conclusion
Custom aluminum extrusion manufacturers combine material science, die engineering, controlled processing, and secondary fabrication to produce profiles tailored to specific applications. The strongest results come from treating design, alloy selection, tooling, extrusion, finishing, and inspection as connected stages rather than isolated decisions.
A carefully developed profile can integrate structural and functional features while supporting repeatable manufacturing across many industries. By evaluating geometry, material properties, tolerances, surface requirements, and downstream fabrication from the start, engineering teams can develop aluminum extrusions that are both practical to manufacture and well matched to their intended application.
Related Post...
Enterprise Endpoint Detection and Response Explore Threat Monitoring
Updated: September 07, 2026
Read More
Optimization Consulting: Explore Strategies for Better Business Efficiency
Updated: August 27, 2026
Read More
Supply Chain Management Systems: Explore How Modern Networks Connect
Updated: September 15, 2026
Read More